Wear plates, parts
& reconditioning.
Steel plates carrying a hard, wear-resistant overlay, applied by flux-cored wire welding, fabricated into finished systems, and reconditioned on a turnkey basis.
Plates & pipes,
off the shelf.
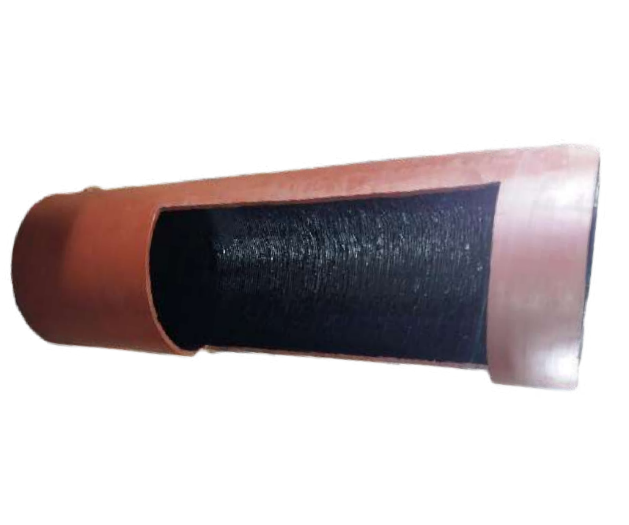
Standard wear-overlay plates and clad pipes in a wide range of base-plus-overlay thicknesses. Dual-side cladding and custom combinations available on request.
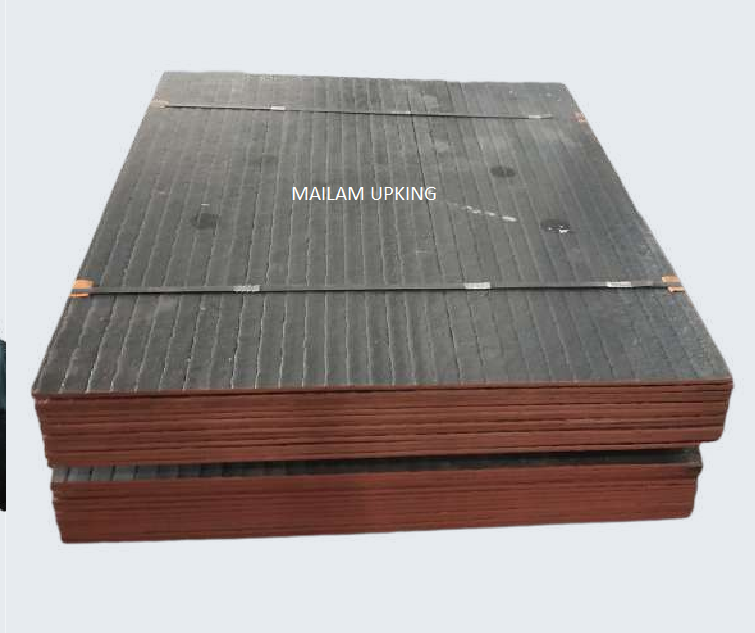
Standard Size Wear Plates
Standard overlay plate stock: width × length in mm, with the available base + overlay thickness combinations.
| Width (mm) | Length (mm) | Thickness: base + overlay (mm) |
|---|---|---|
| 1150 | 4900 | 4+2, 5+3, 6+4, 8+4, 8+5, 10+4, 10+5, 10+6, 12+4 |
| 1400 | 3050 | 4+2, 5+3, 6+4, 8+4, 8+5, 10+4, 10+5, 10+6, 12+4 |
| 1900 | 3050 | 4+2, 5+3, 6+4, 8+4, 8+5, 10+4 |
| 1300 | 2900 | 4+8+4 (dual-side clad, any combination) |
| 1300 | 2900 | 10+4 to any combination |
| 1900 | 6100 | Min - 3+3mm to Upto 10+6mm Any Combination |
| 1400 | 6100 | Min - 3+3mm to Upto 10+6mm Any Combination |
Standard Size ID & OD Cladded Pipes
Standard cladded pipe sizes: overlay-on-base cladding in mm, with inner / outer diameter × length.
| Cladding (mm) | Inner Ø × L | Outer Ø × L |
|---|---|---|
| 4 on 6 | 0.2 m × 1 m | 0.1 m × 1 m |
| 4 on 6 · 5 on 8 | 0.25 m × 1 m | 0.15 m × 1 m |
| … · 6 on 6 | 0.3 m × 1 m | 0.2 m × 1 m |
| … · 5 on 10 | 0.35 m × 1 m | 0.25 m × 1 m |
| … · 6 on 8 | 0.4 m × 1 m | 0.3 m × 1 m |
| … · 8 on 10 | 0.5 m × 1 m | 0.4 m × 1 m |
| … · 8 on 10 (heavy) | 0.6 m × 1 m | 0.5 m × 1 m |
Composite wear-plate assemblies to 18 on 20 and custom dual-side cladded plates available. Talk to our engineering team.
Manufactured &
reconditioned.
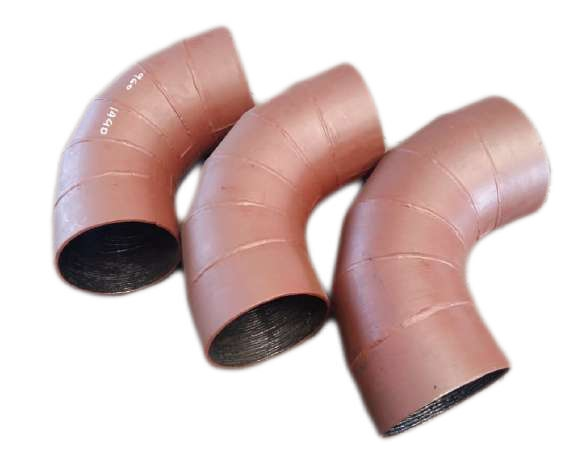
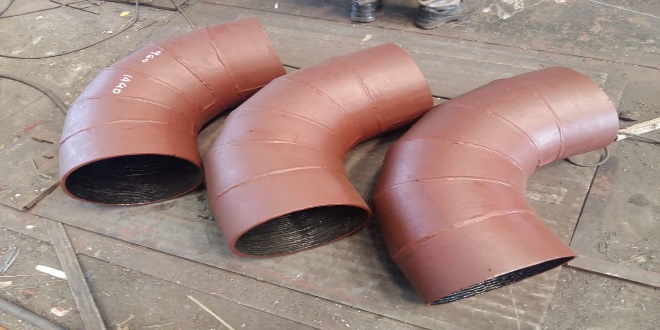
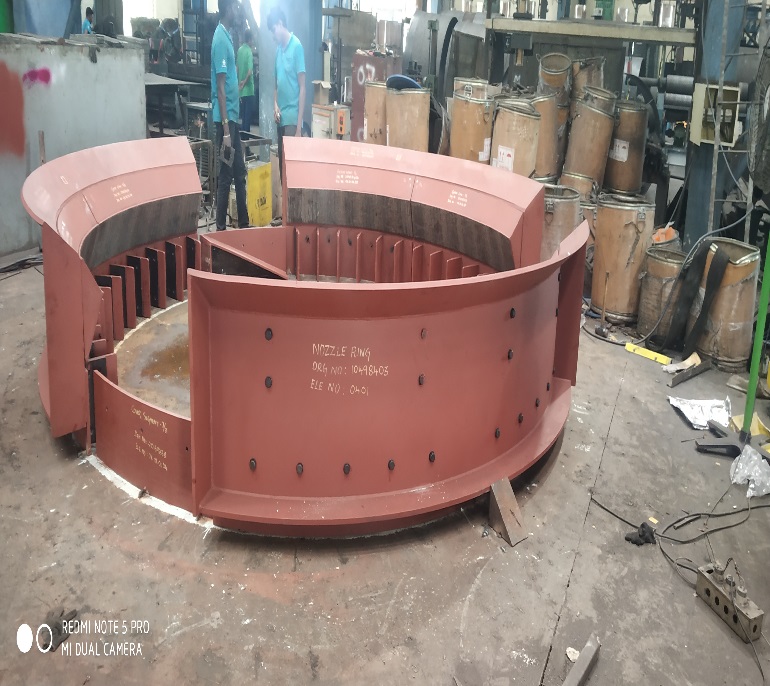
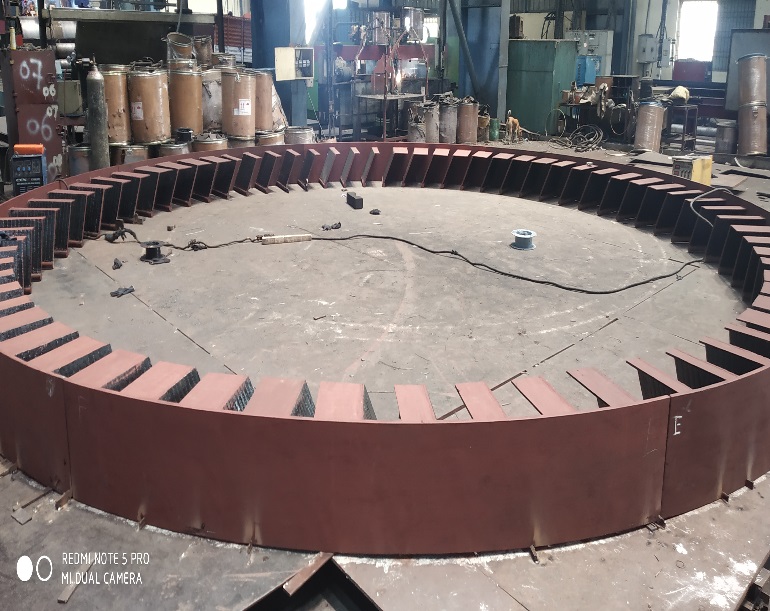
A comprehensive range of industrial wear parts, manufactured new or reclaimed to original specification. Click any image to enlarge.
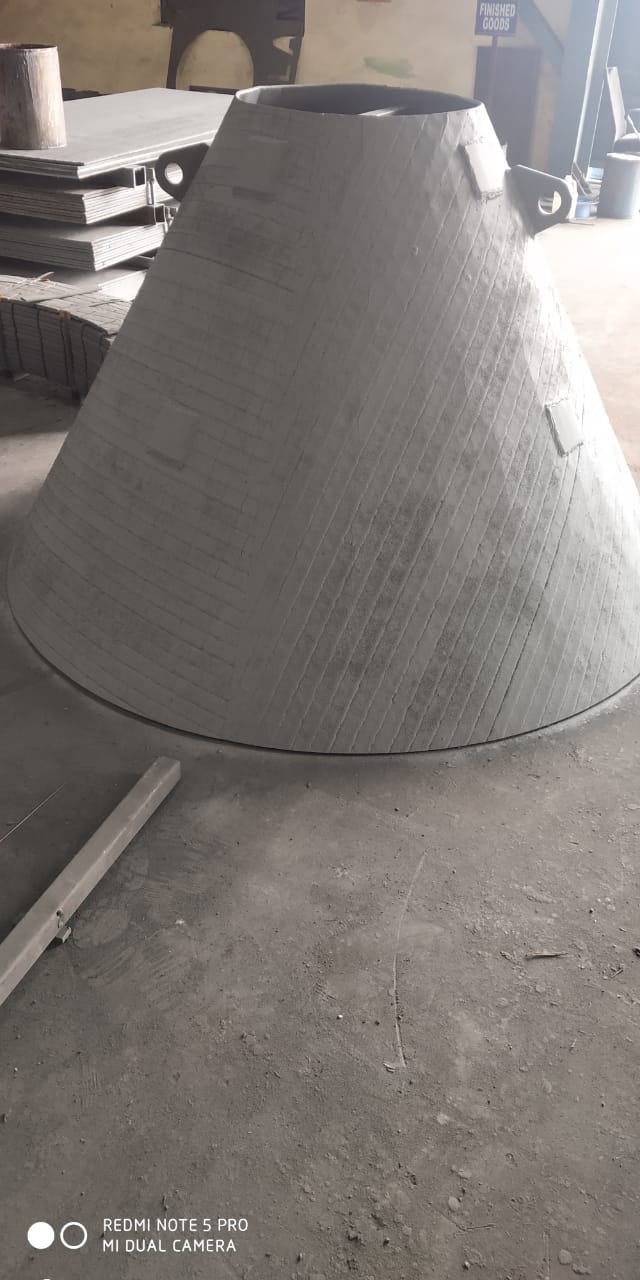
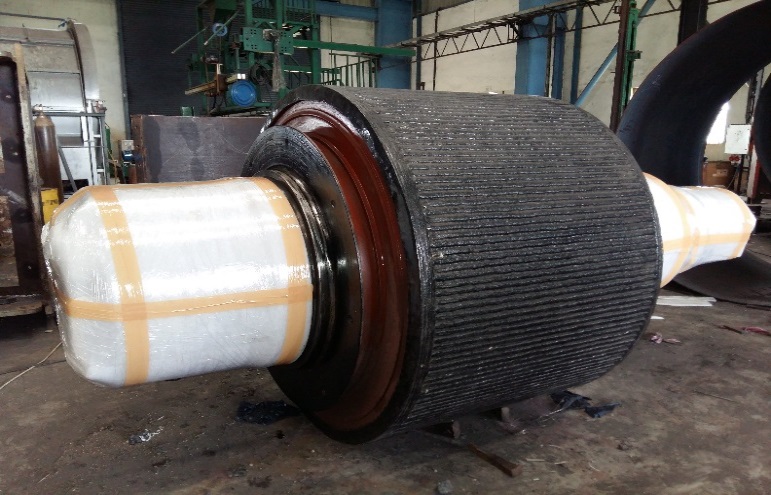
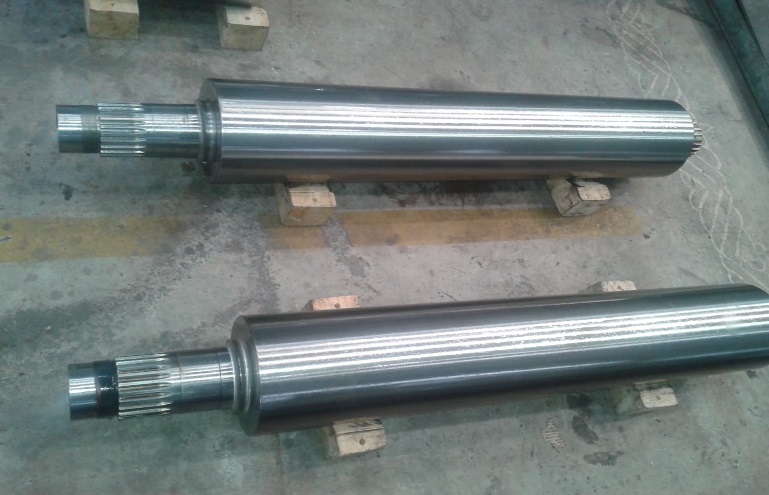
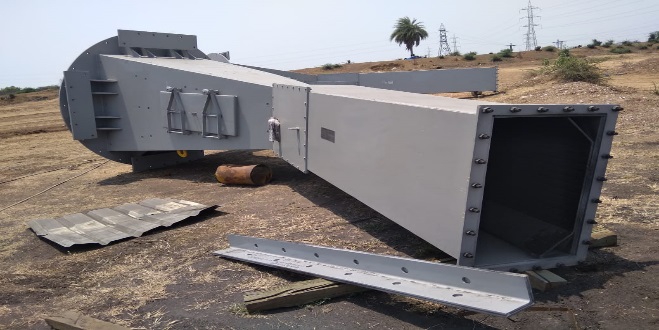
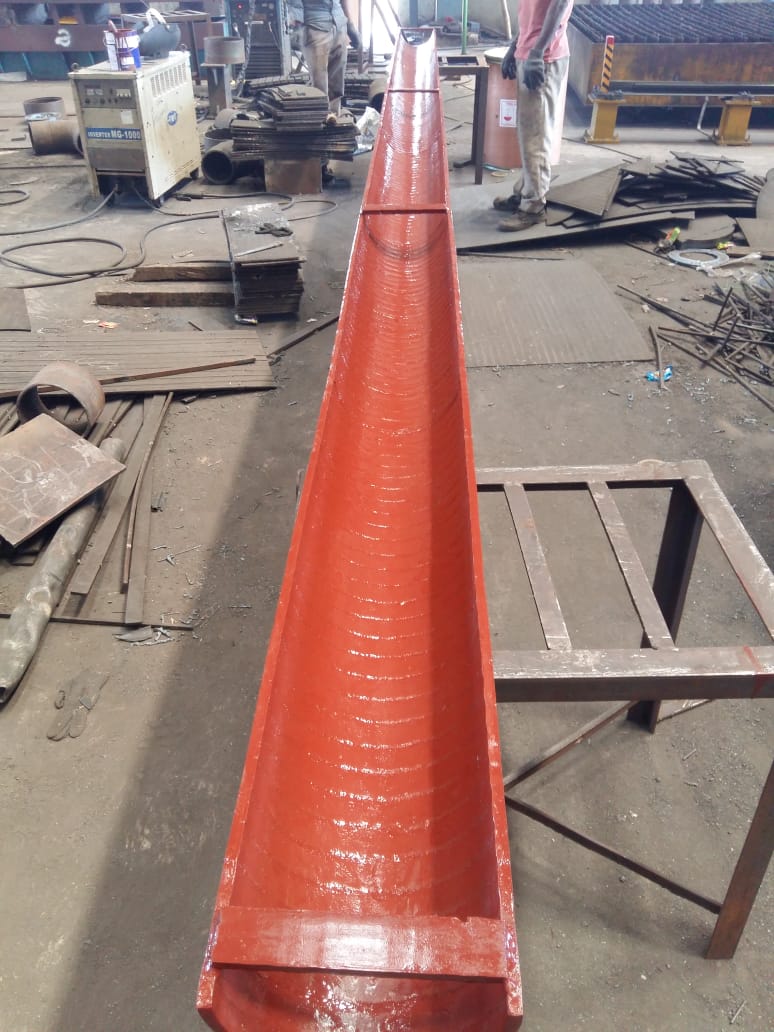
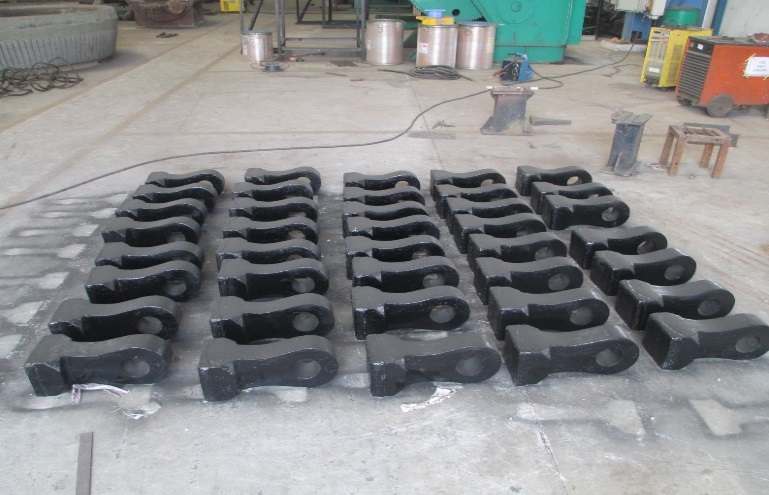
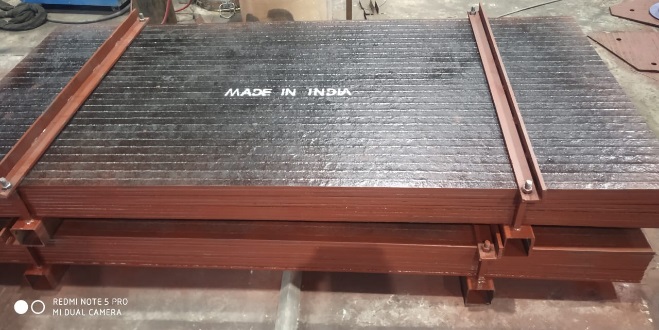
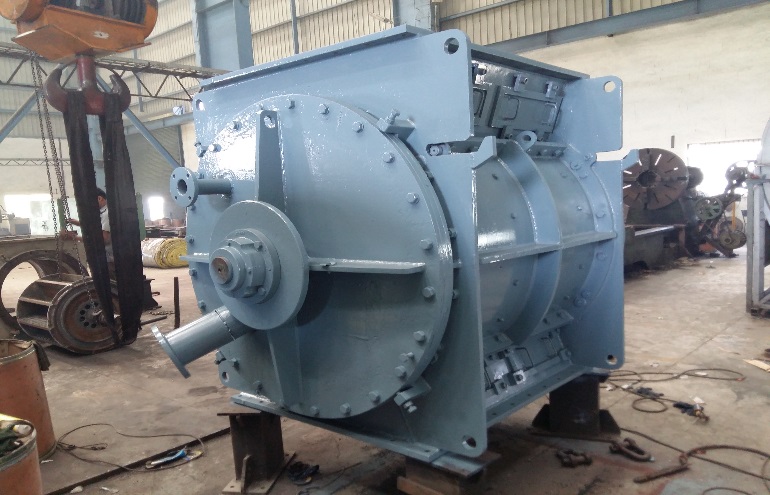
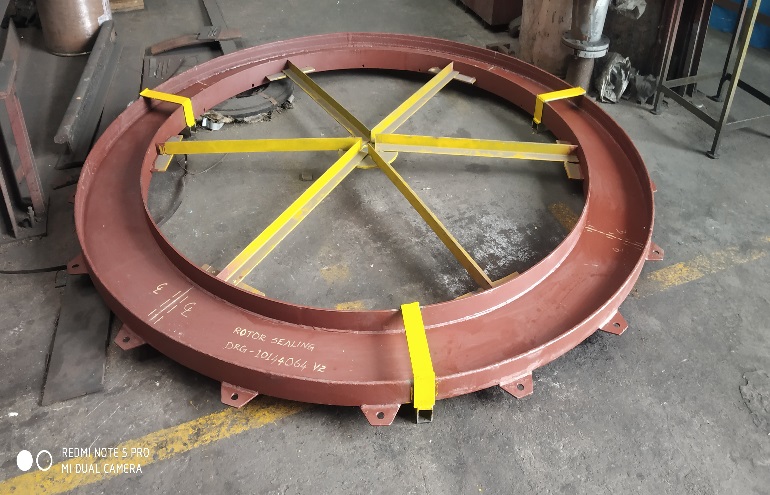
Full parts range
Don’t see the part you need? We manufacture and recondition to your drawing and service condition.
More products / customise →Reconditioning service at
on-site or off site.
A full-fledged workshop equipped to take up any kind of welding repair or re-building job on a turnkey basis, in the plant or at your site.
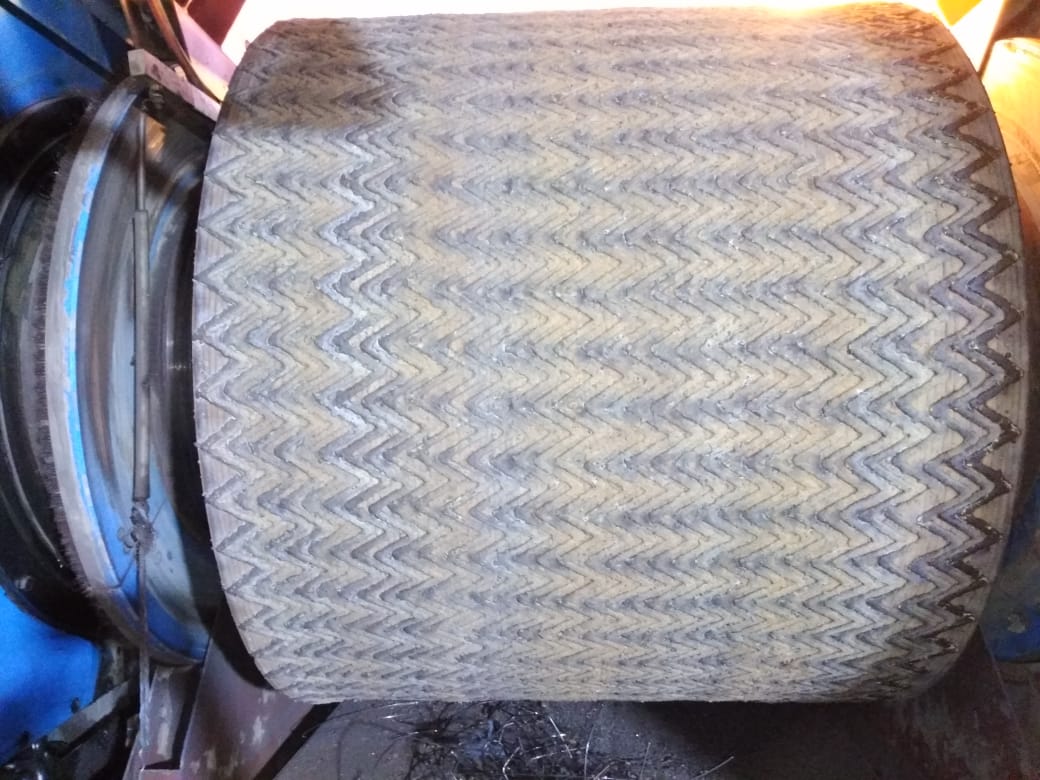
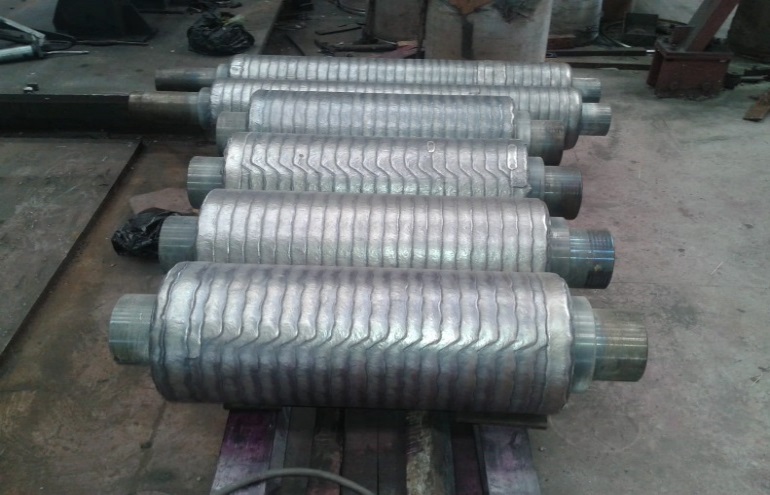
Reconditioning & Hardfacing
Rebuilding worn rollers, tyres, table liners and rotating equipment to original profile and hardness, extending service life at a fraction of replacement cost.
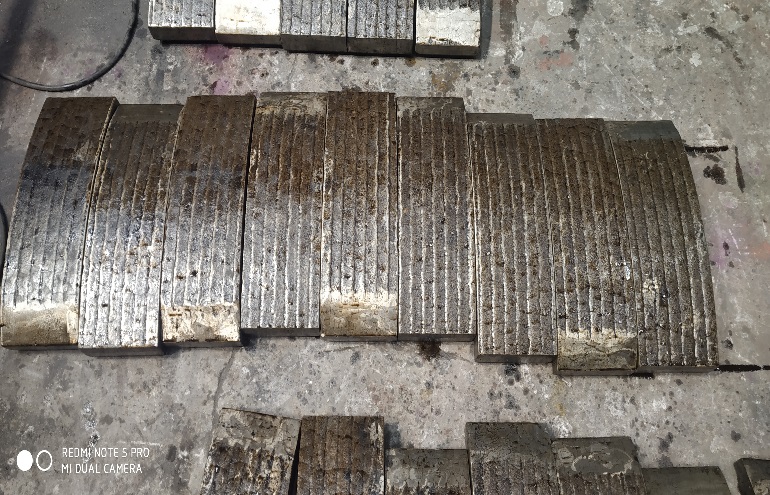
Custom Wear Engineering
Our R&D develops custom-made overlay compositions to meet specific application needs, wear-resistant liner solutions designed around your service condition.
Rebuild the mill,
without pulling it out.
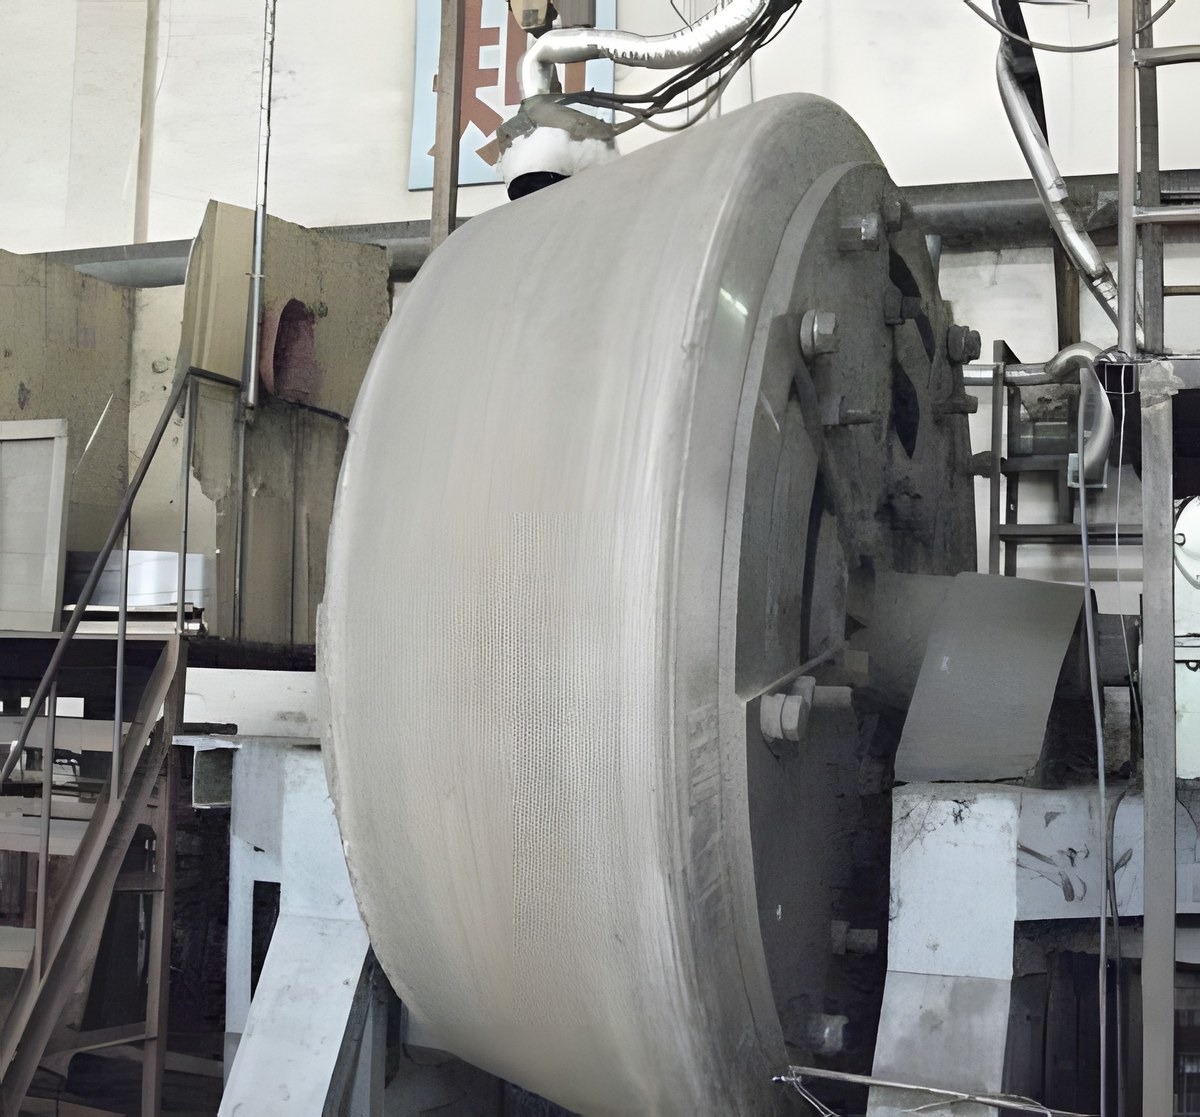
VRM grinding rollers, table liners and roller-press rolls wear down and need re-cladding over time. Our online hardfacing system (and our MOA build-up and surfacing wires) rebuild them in place: no dismantling, minimal downtime.
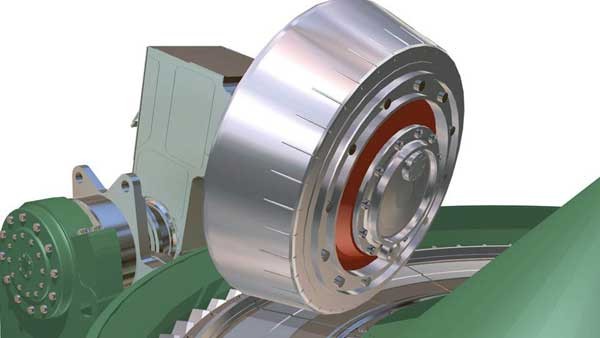
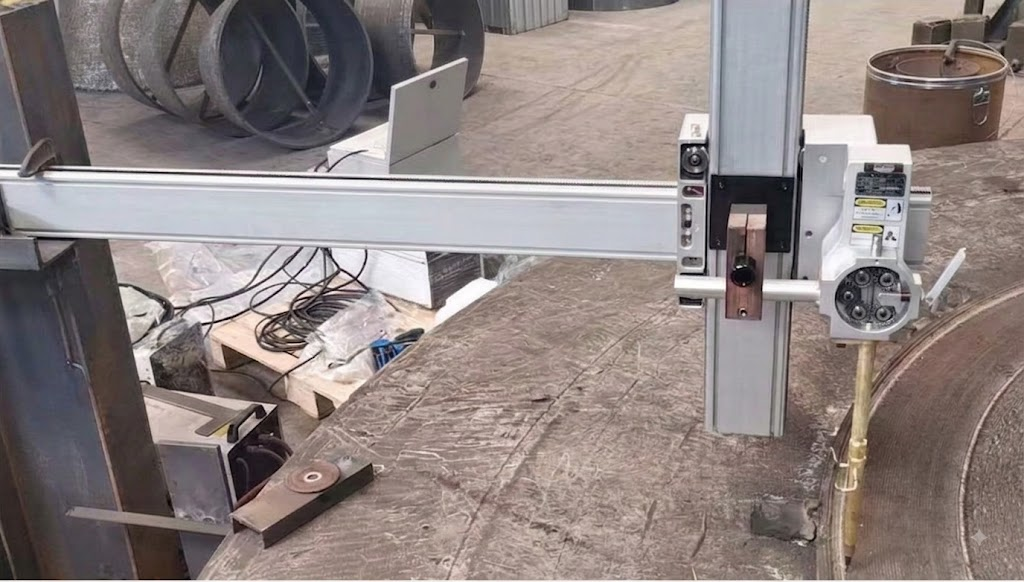
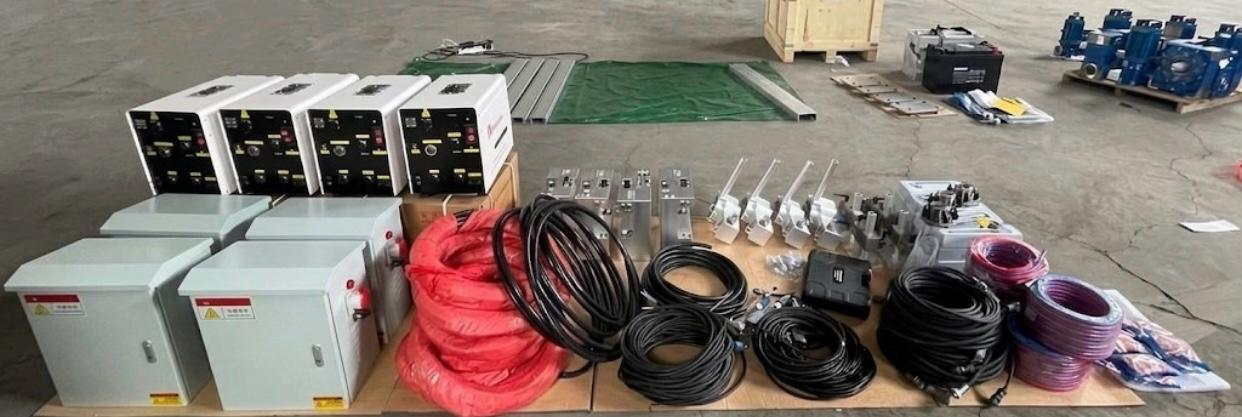
Our VRM Hardfacing system mounts an X/Y column-boom rig directly onto the mill and rebuilds worn roller sleeves and grinding-disc linings with flux-cored overlay while the parts stay in place, online or offline. The complete system spans the grinding-roller drive, welding-gun travel mechanism, dust-cleaning device, welding machine, and power-supply & control cabinets, run from a PLC/HMI for continuous, repeatable cladding.
- Processes
- Open arc · submerged arc · flux & gas-shielded arc welding
- Rig & motion
- X/Y column boom · 145 mm aluminium beam (custom length) · high-accuracy cross tractor
- Wire feed
- 1.6–3.2 mm flux or solid wire · 4-roller straightener · 2–9 m/min
- Power source
- 1000 A at 100% duty cycle · CC/CV · 24 h continuous
- Mill drive
- Drive motor, reducer & converter rotate the roller / table during cladding
- Cooling & earth
- 10 L water cooler (~20 m tube) · 360° rotating grounding
- Control
- PLC/HMI strip / grid / spot cladding · auto air-gouging · handheld remote · usage logging
The assembled system, annotated.
The complete VRM Hardfacing rig as it ships. Hover or tap the numbered points to identify each part of the assembly.
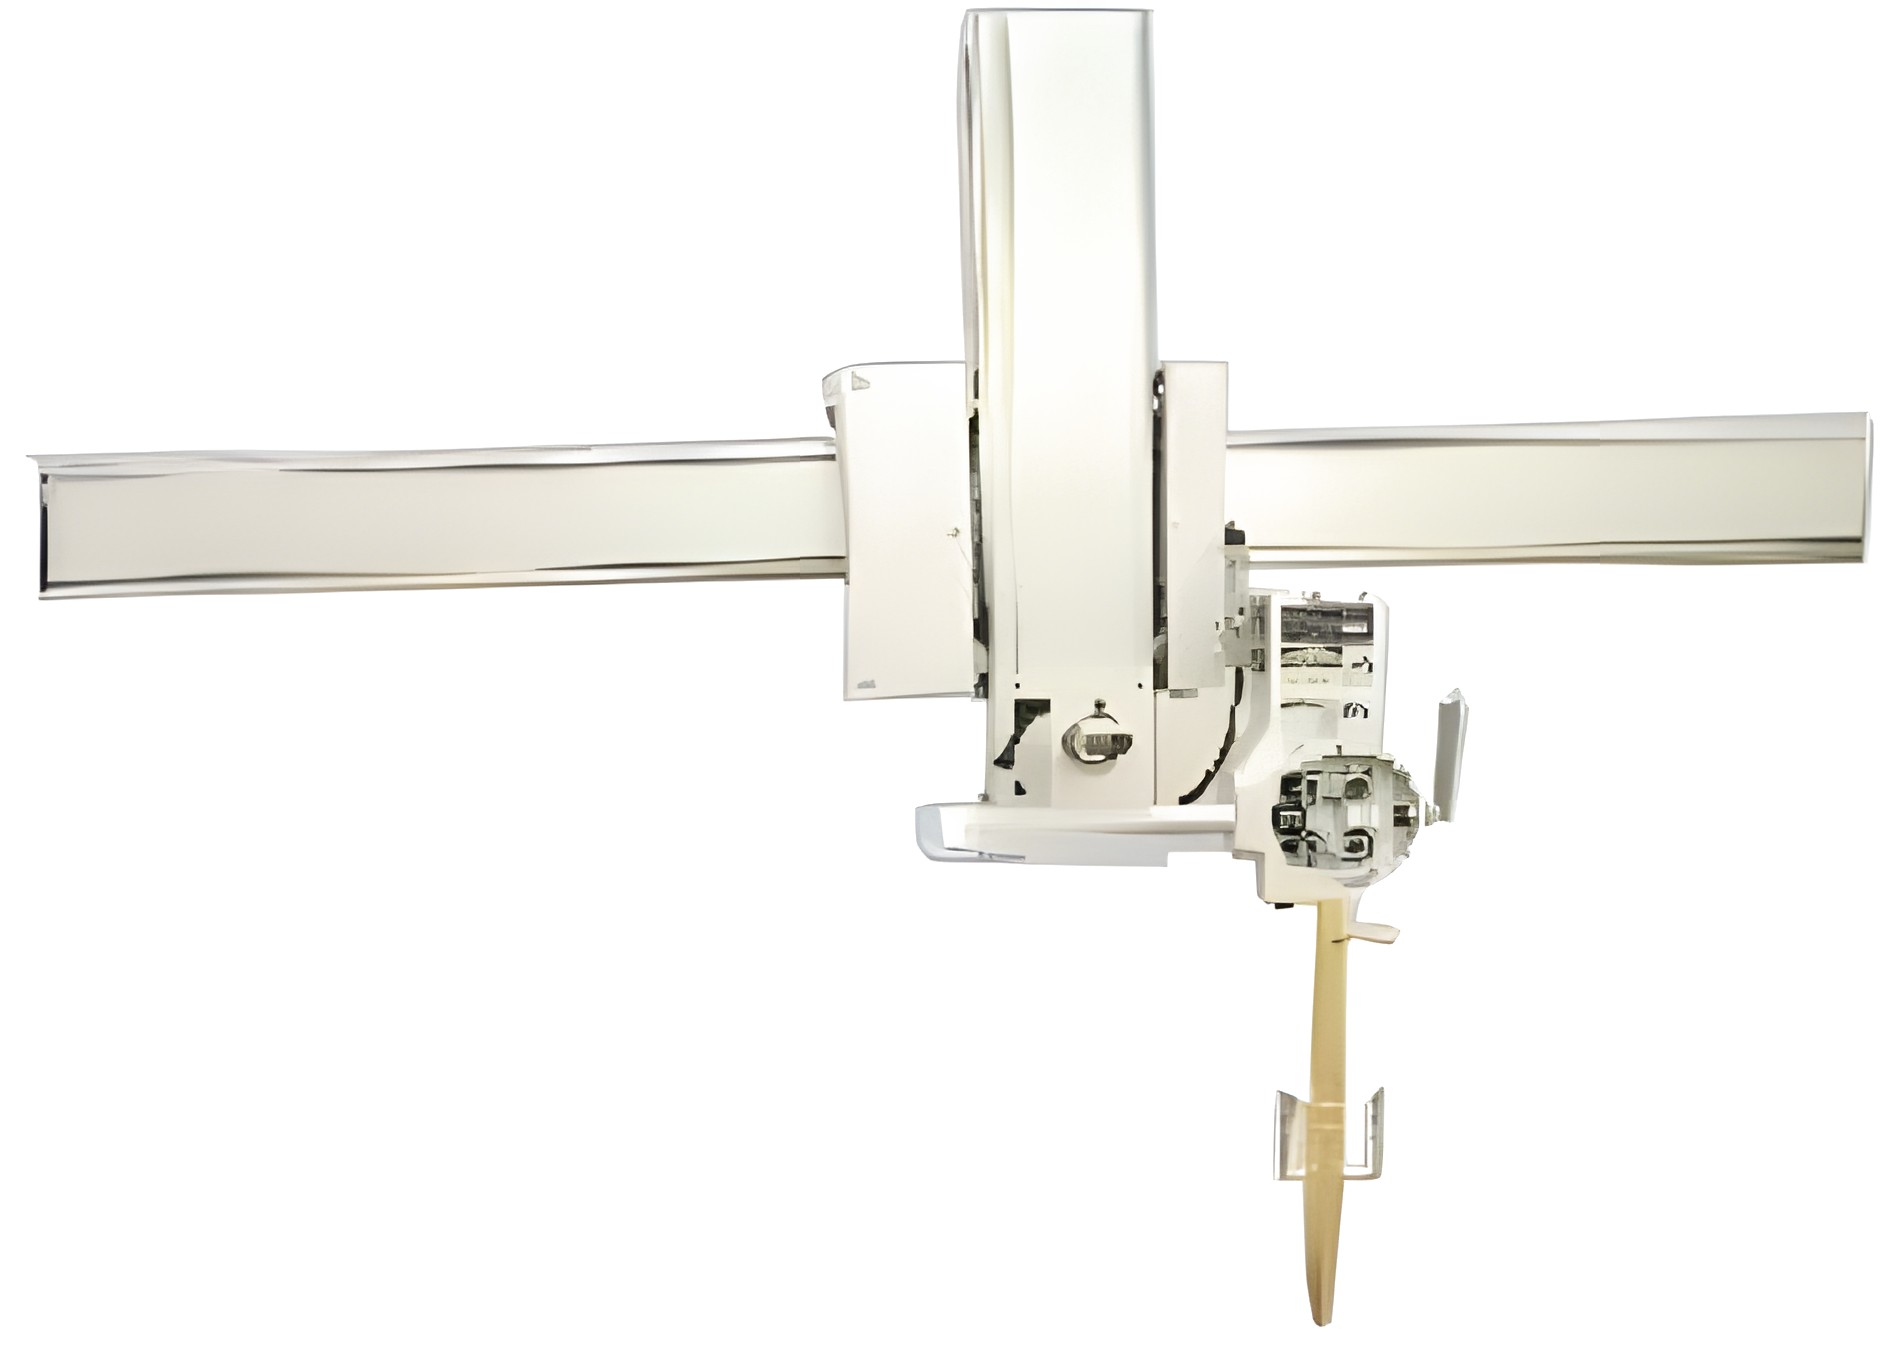
Y-Axis Beam
Vertical aluminium arm. Stepping lift controls the torch reach.
Travelling Cross Tractor
High-accuracy X/Y stepping so the torch reaches every point.
X-Axis Beam
145 mm aluminium travel rail: custom lengths, quick-mount.
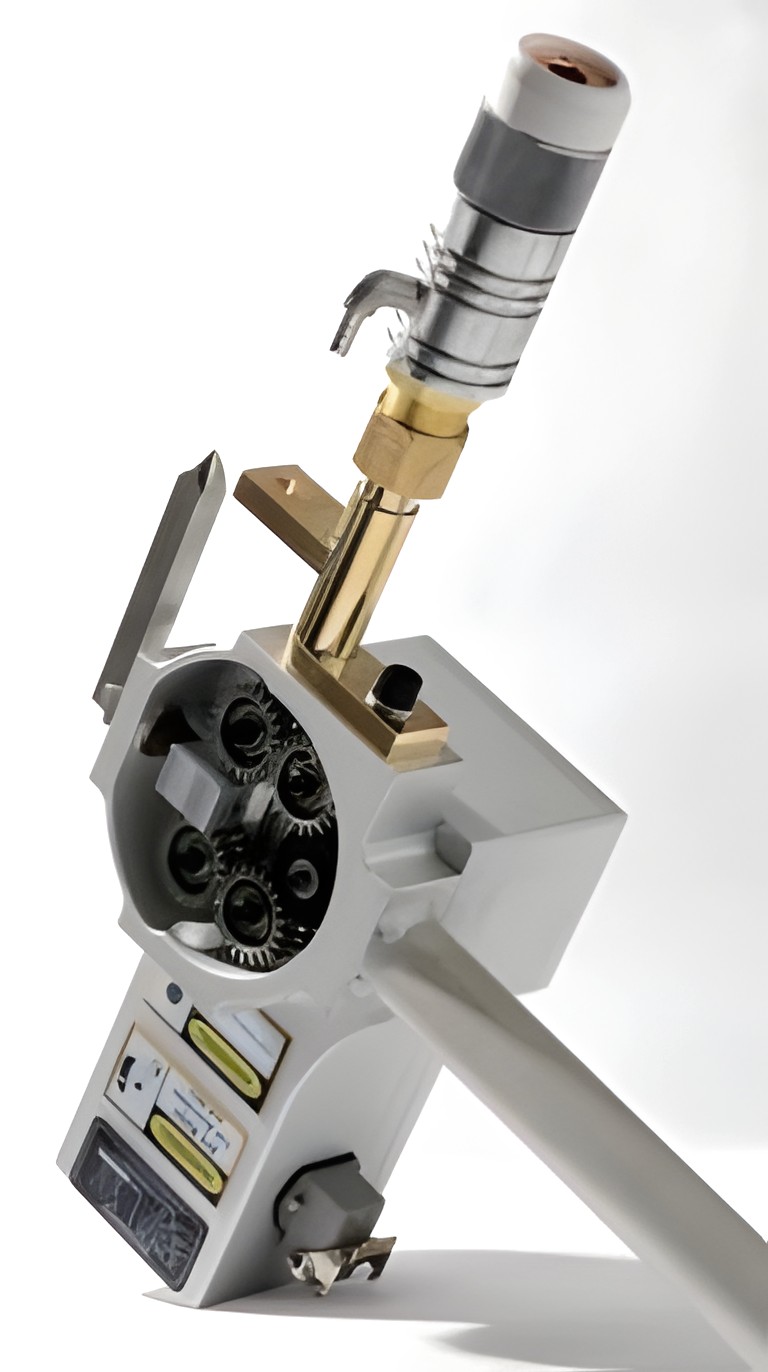
Wire Feeder
4-roller straightener · 1.6–3.2 mm flux or solid wire · 2–9 m/min.
Water-Cooled Torch
Runs continuously off the 10 L water-cooling loop.
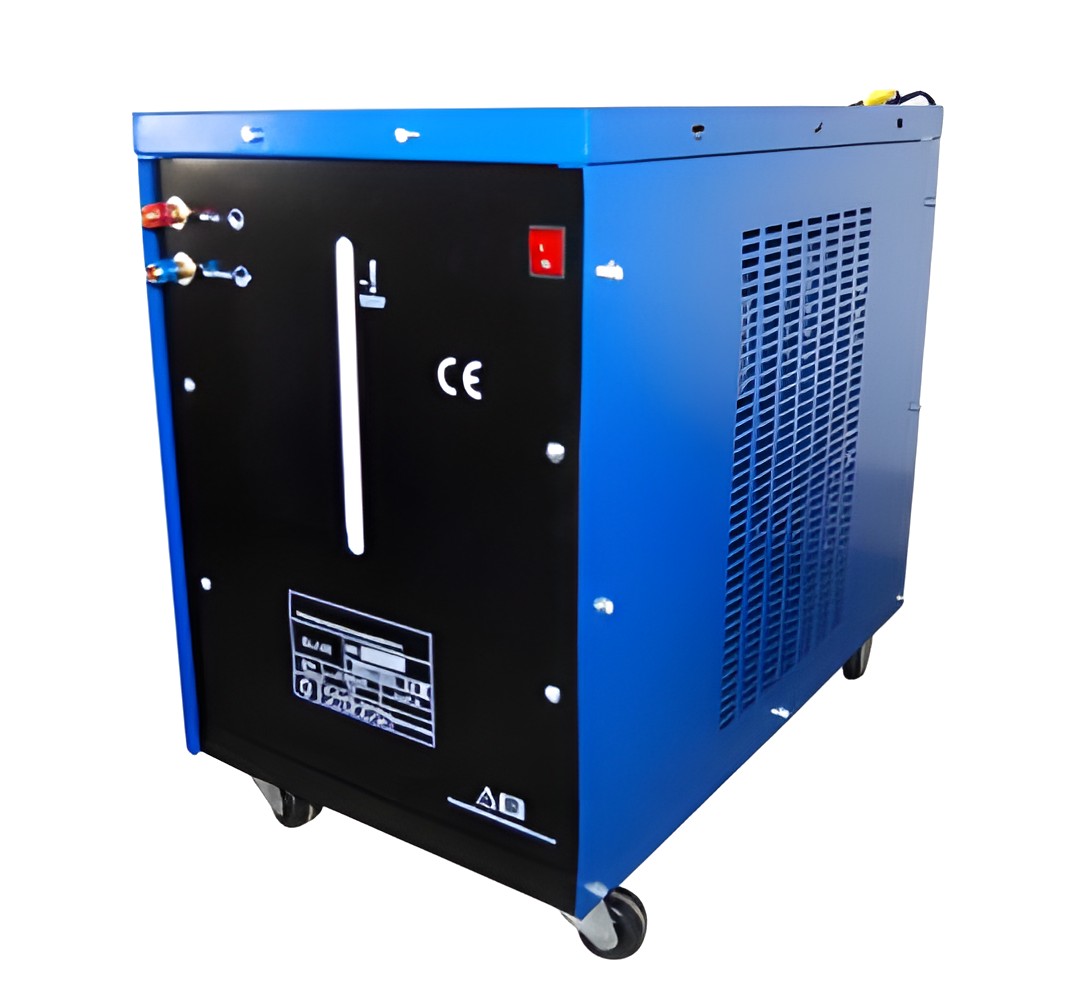 Water Tank
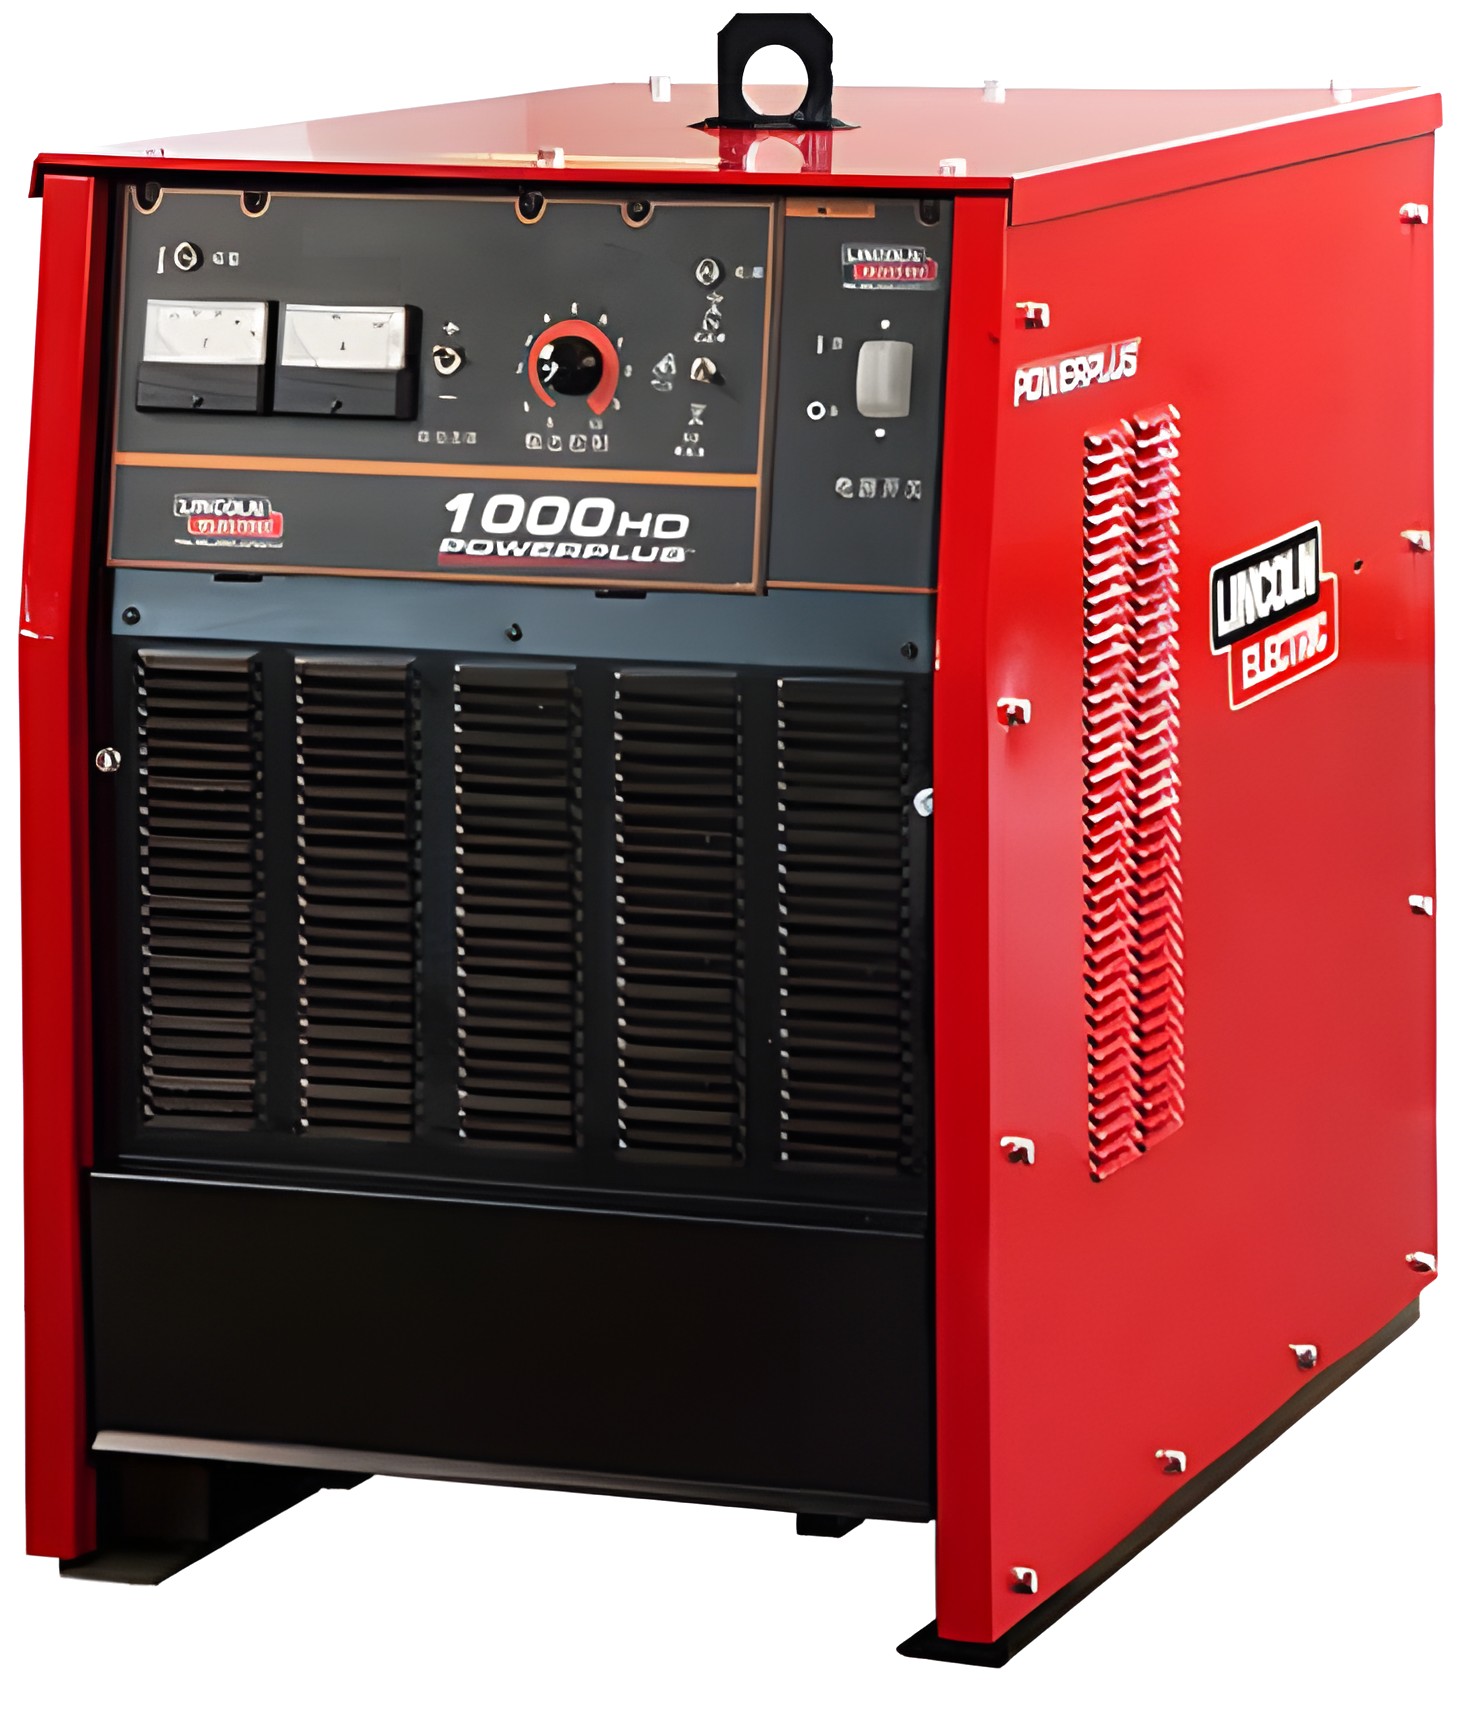 Power Source
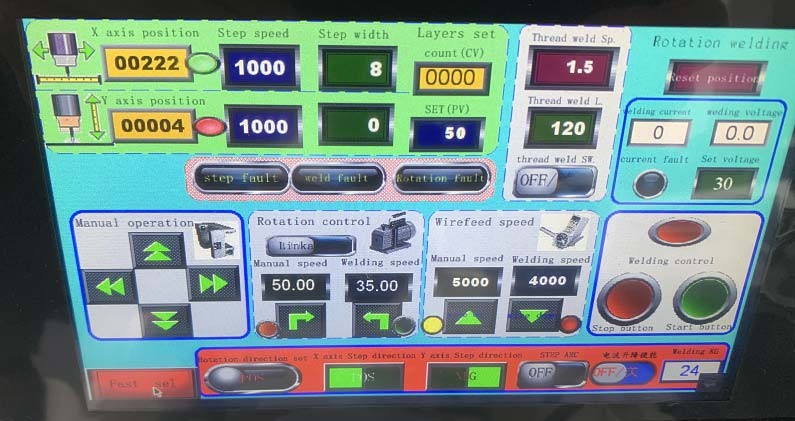 PLC / HMI
Inside the system, part by part.
Every part of the VRM Hardfacing rig (from the column boom to the 360° grounding) with its own spec. Hover a part to preview it; click to enlarge.
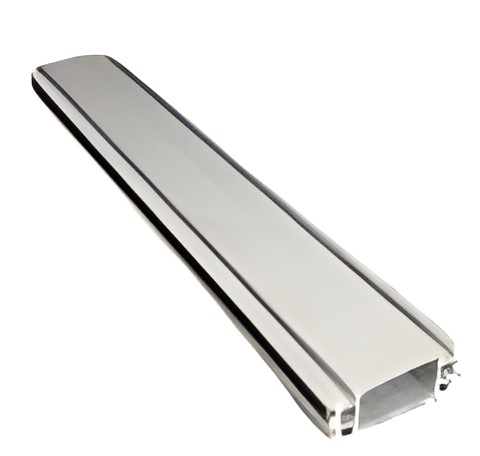 0101 / 11X/Y Axis Beam
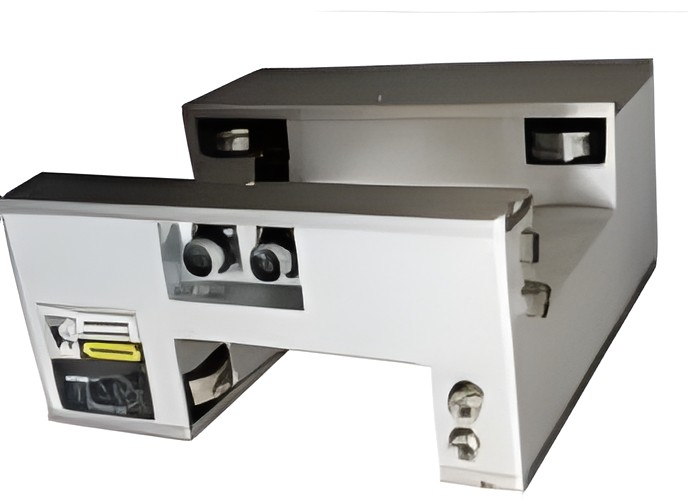 Cross-Travelling Tractor
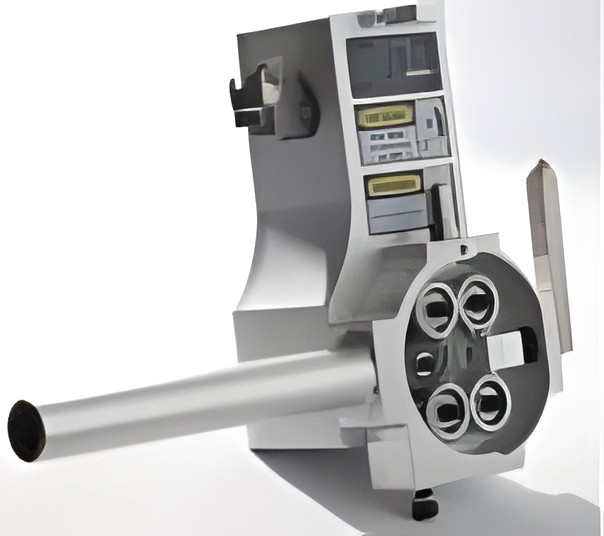 Wire Feeder
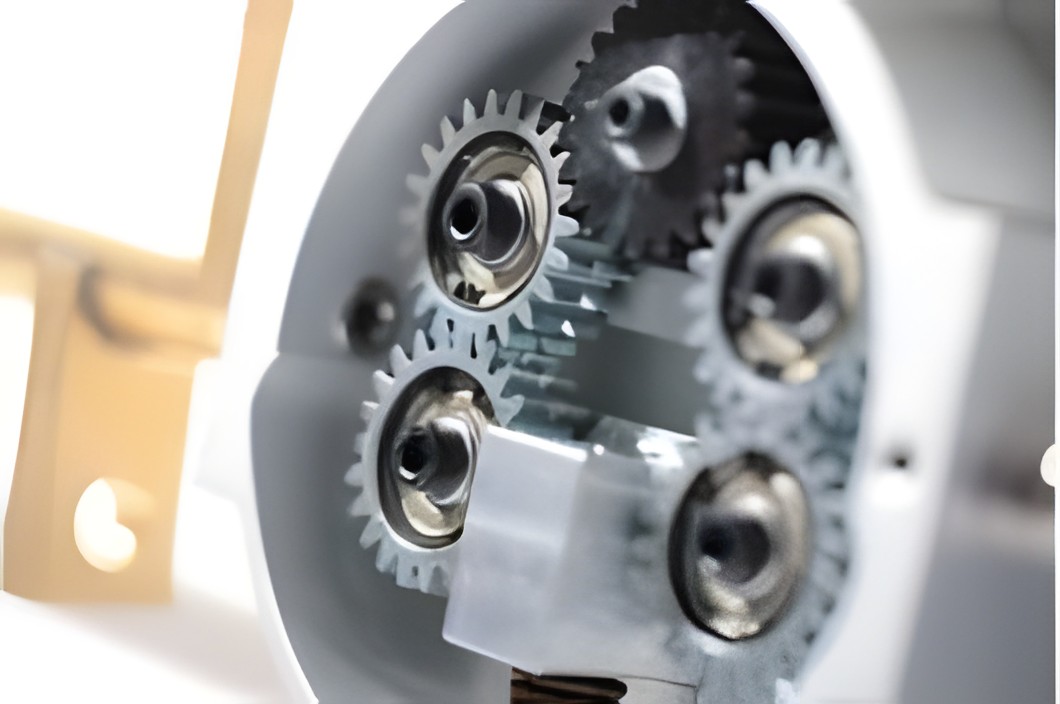 Wire Feeding RollerWelding Power Source
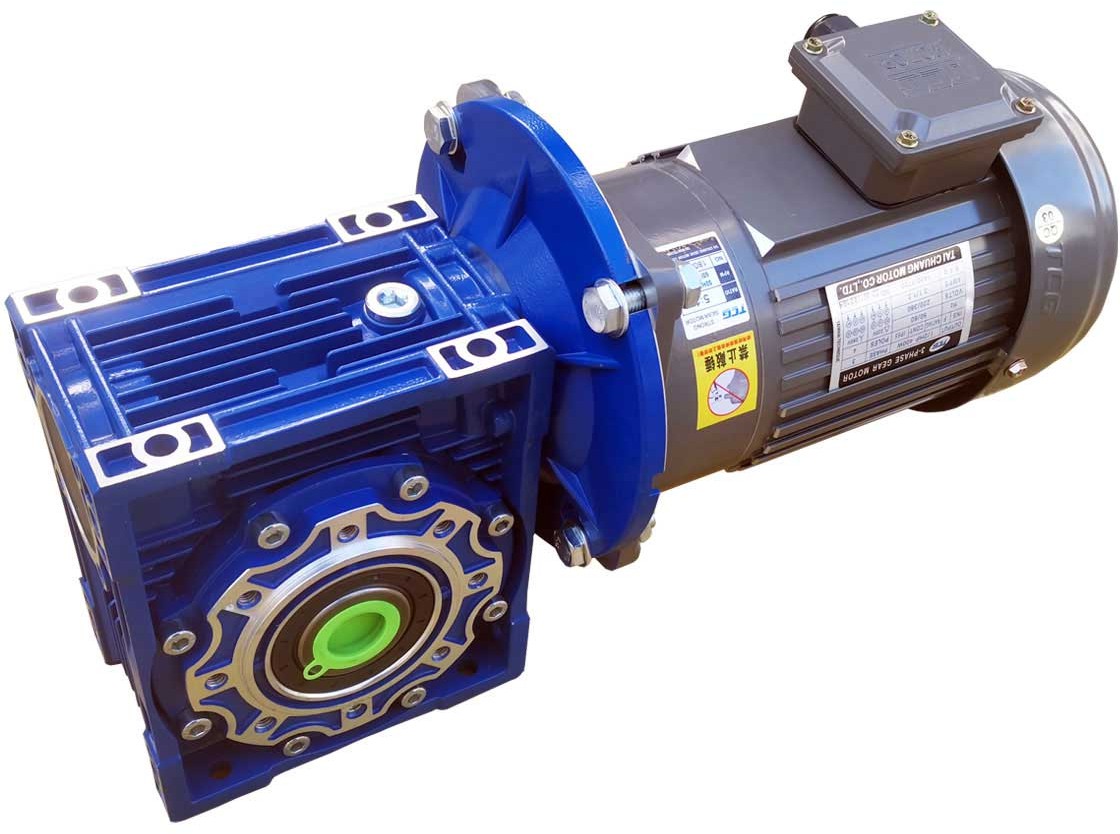 Mill & Table Drive
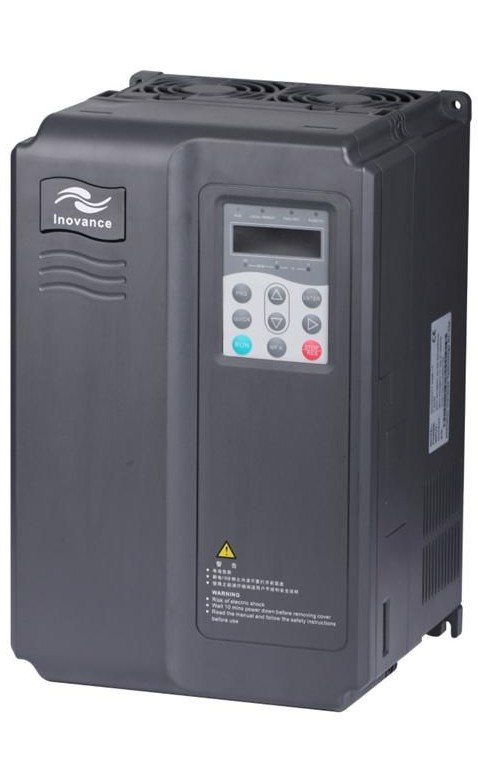 Drive Control Converter
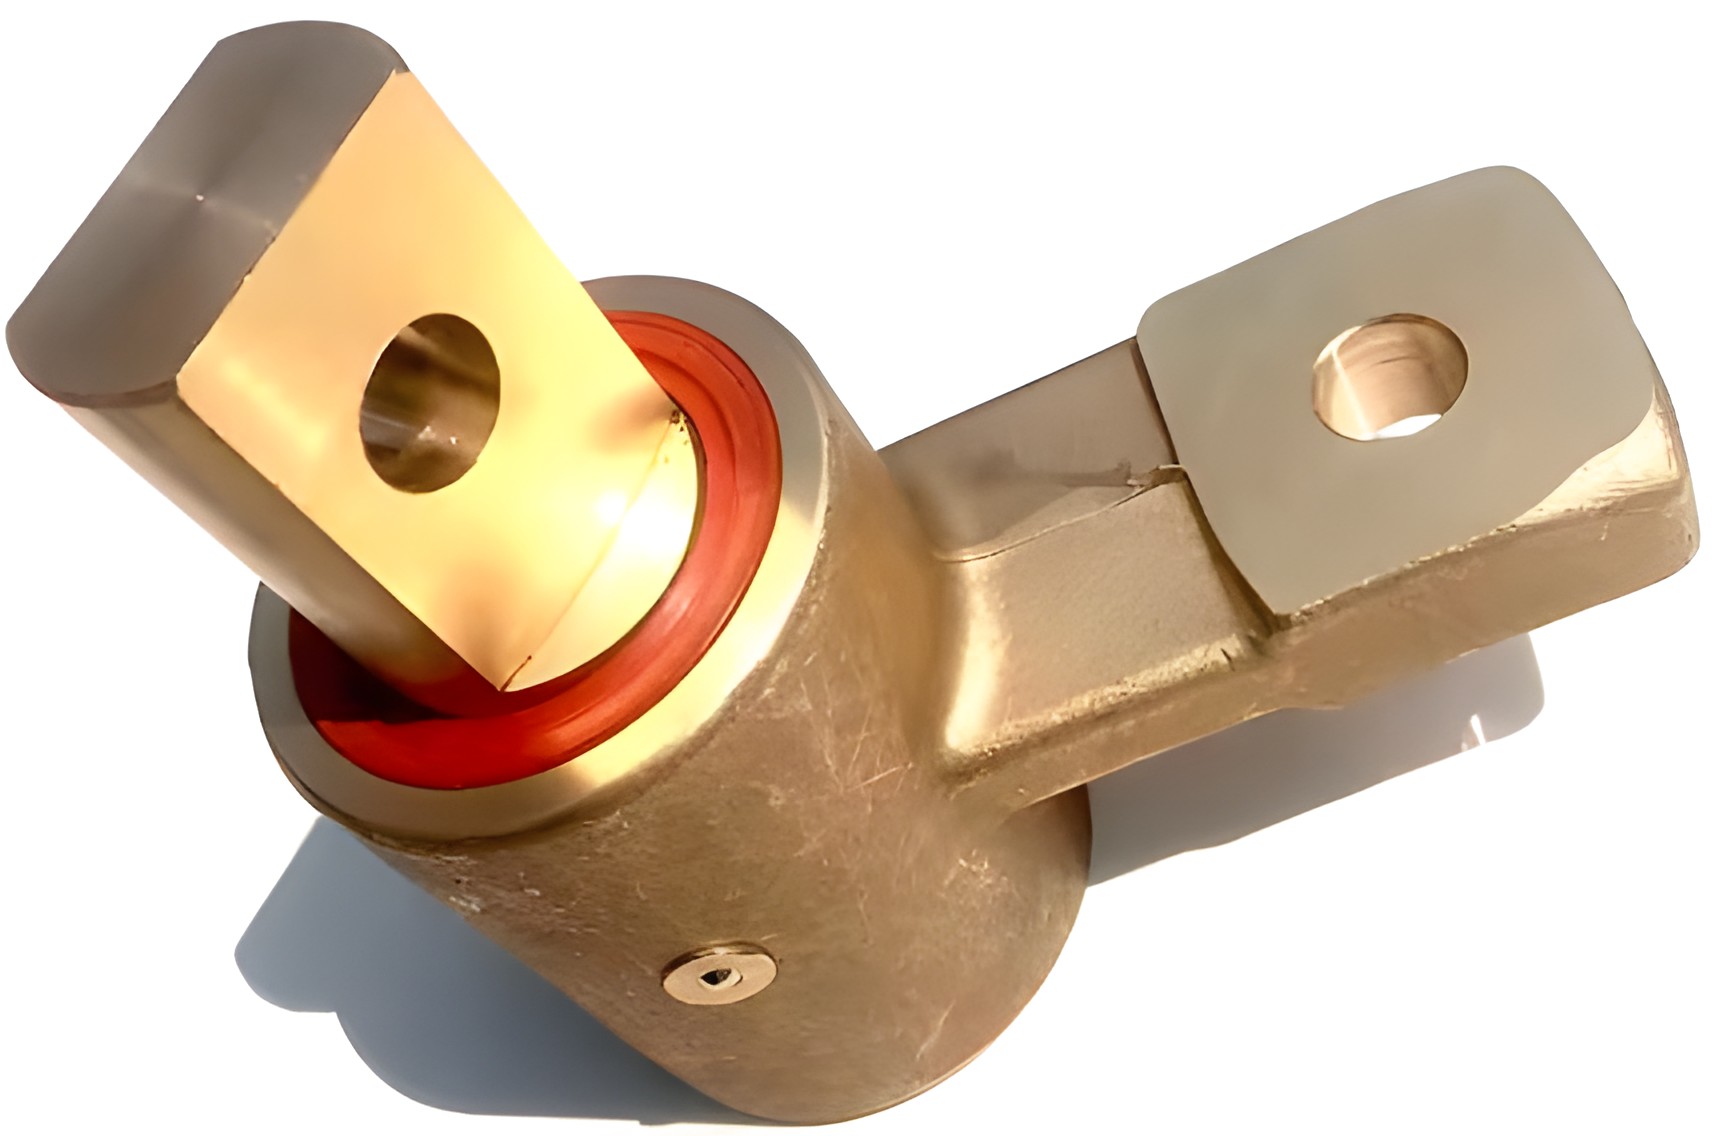 360° Rotating Grounding
 Gouging Torch (Optional)Water CoolerPLC / HMI Control
How it sets up on your mill.
The whole system installs around the mill without dismantling it: four steps from mounting to the first cladding pass.
Mount the boom
Quick-mount the X/Y column boom at the roller, in the mill (online) or on a 'U'-shape steel fixture (offline).
Drive the rotation
Drive motor, reducer and the 380 V control converter turn the roller or table at a steady cladding speed.
Ground & power
360° rotating grounding and the 1000 A output cable close the welding circuit while the part turns.
Clad from the HMI
The quick-plug PLC touchscreen (or handheld remote) runs strip / grid / spot programs and logs wire and arc time.
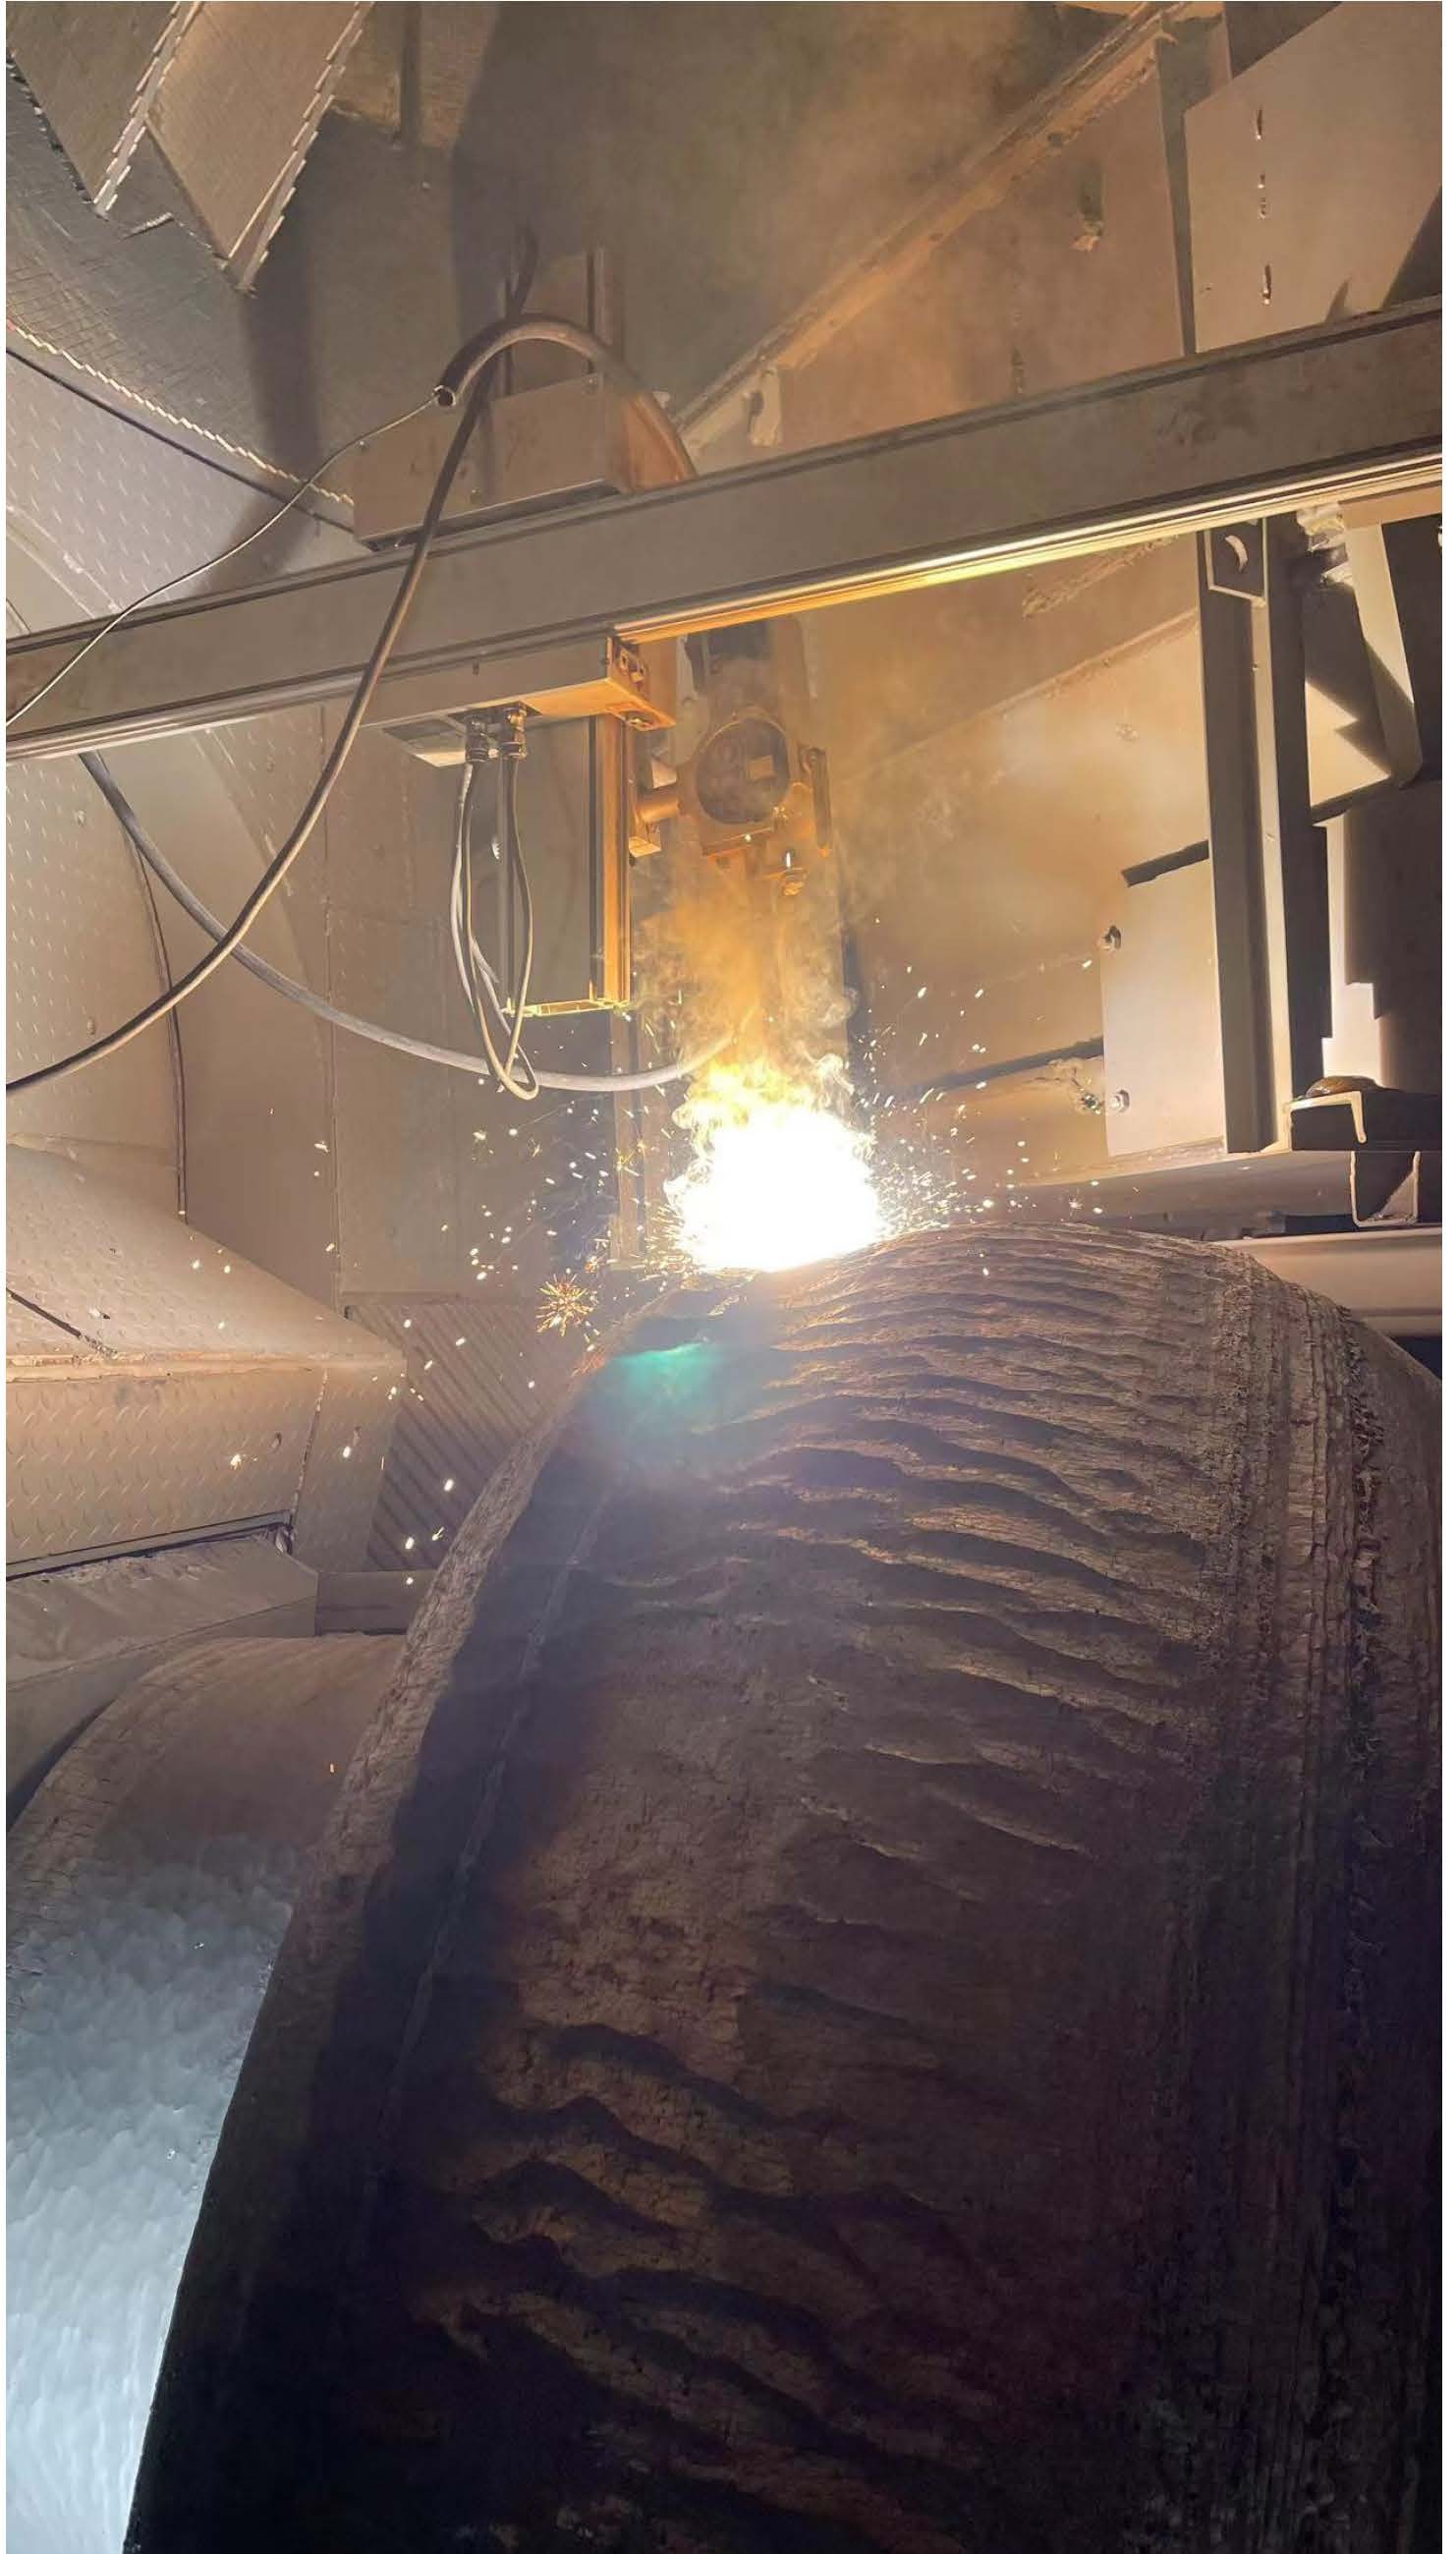
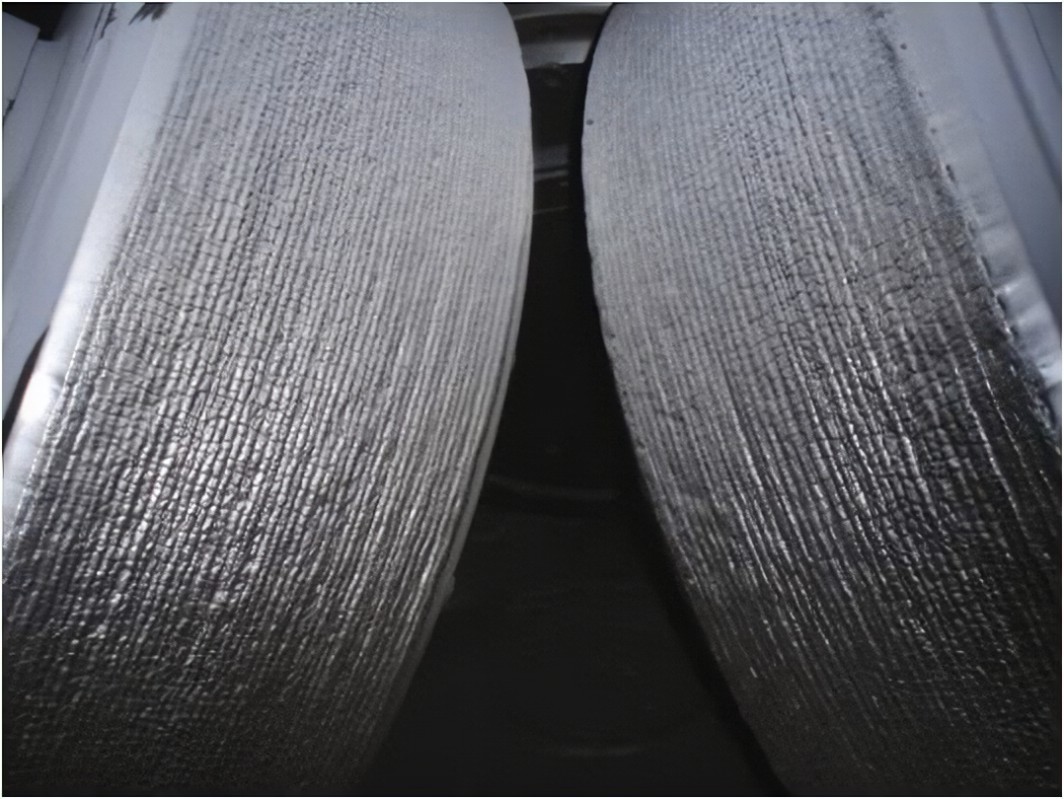
The final output, in the mill.
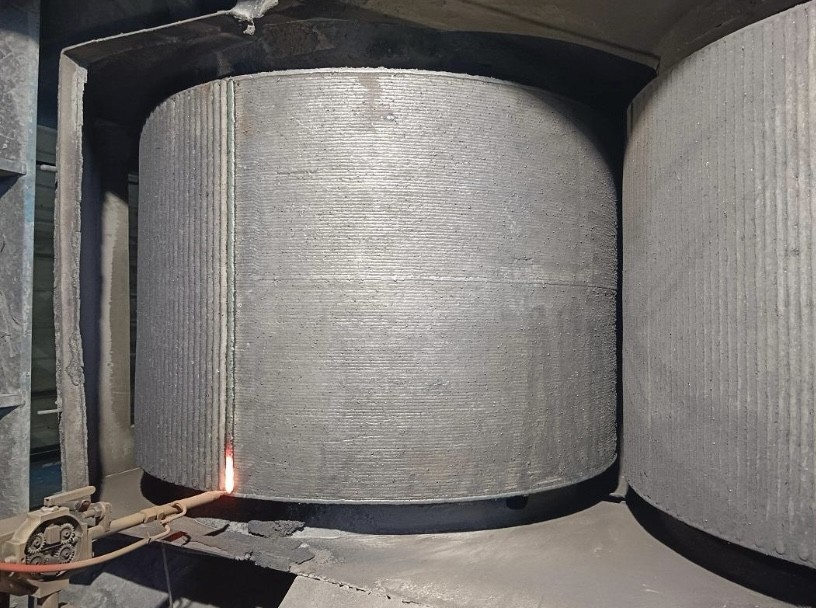
2.8 mm open-arc flux-cored overlay laid layer by layer while the roller turns, rebuilt in place, with no dismantling and no transport.
A two-wire system: rebuild, then armour.
Worn rolls and tables are first restored to profile with an MOA-506 build-up layer, then armoured with an MOA-507 hard surface layer, the same drum-packed wires run through our online rig.
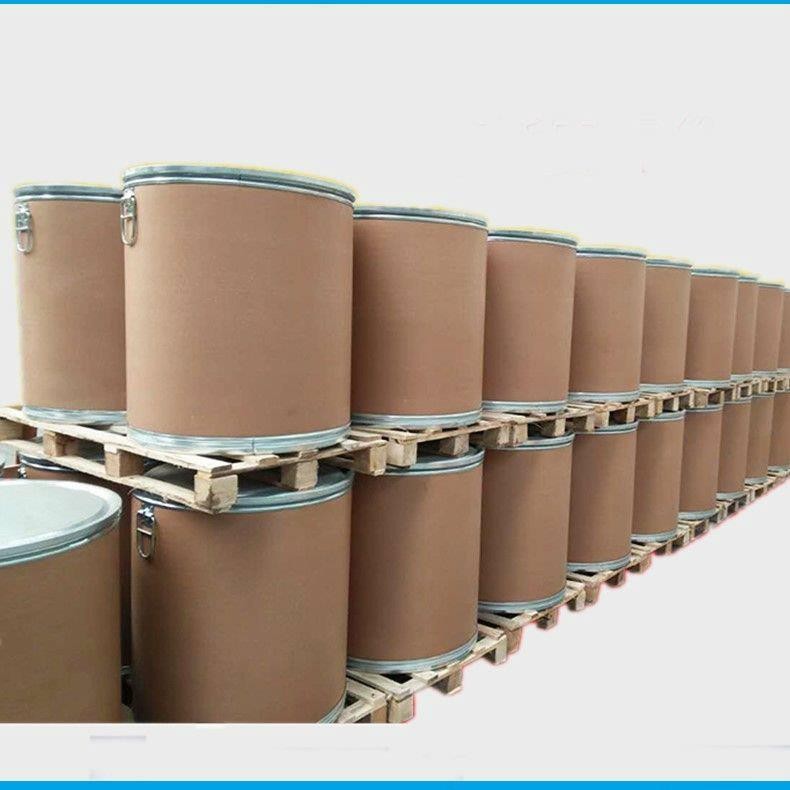
Flux-cored build-up wire for the repair and remanufacture of coal grinding rolls and grinding disks, good wear resistance with the toughness to take high-hardness mineral particles.
- Wire diameter
- 2.4 / 2.8 mm
- Chemistry (%)
- C 4.0–5.5 · Cr 25–30 · Mn 0.4–0.8 · Mo 0.8–1.4 · Si 1.0–1.8 · Fe bal.
- Hardness
- 58–61 HRC
- Process
- FCAW open arc · 300–550 A · 28–35 V
- Interpass temp
- Each layer controlled within 100 °C
- Packing
- Drum packed · 125 / 250 kg
Used for: Vertical crushers, grinding rollers, conveyor armour, wear plates, screen plates, mud pumps & mixers.
C-Cr-Nb metal-cored hardfacing wire, niobium- and chromium-carbide alloy with excellent resistance to fine, high-hardness abrasives under severe wear and moderate impact.
- Wire diameter
- 2.8 mm
- Chemistry (%)
- C 4.0–6.0 · Cr 18–24 · Mn 0.2–1.0 · Nb 6–8 · Si 0.5–1.0 · Fe bal.
- Hardness
- 62–64 HRC
- Process
- FCAW open arc · 300–550 A · 28–35 V
- Interpass temp
- Each layer controlled within 100 °C
- Packing
- Drum packed · 125 / 250 kg
Used for: Roller-press pattern layer and vertical-mill roller / table hard-surface layers.
Applications: cement vertical mills, coal mills, grinding tables, roller-press rolls & continuous-caster rolls, for cement, power, steel and mining plants.
Enquire about online hardfacing →Electrodes &
welding wires.
The flux-cored wires used across our wear-plate range are manufactured by Mailam Upking itself. Backed by our parent’s lab, we also supply joining and anti-wear electrodes, including ghost-spec grades.
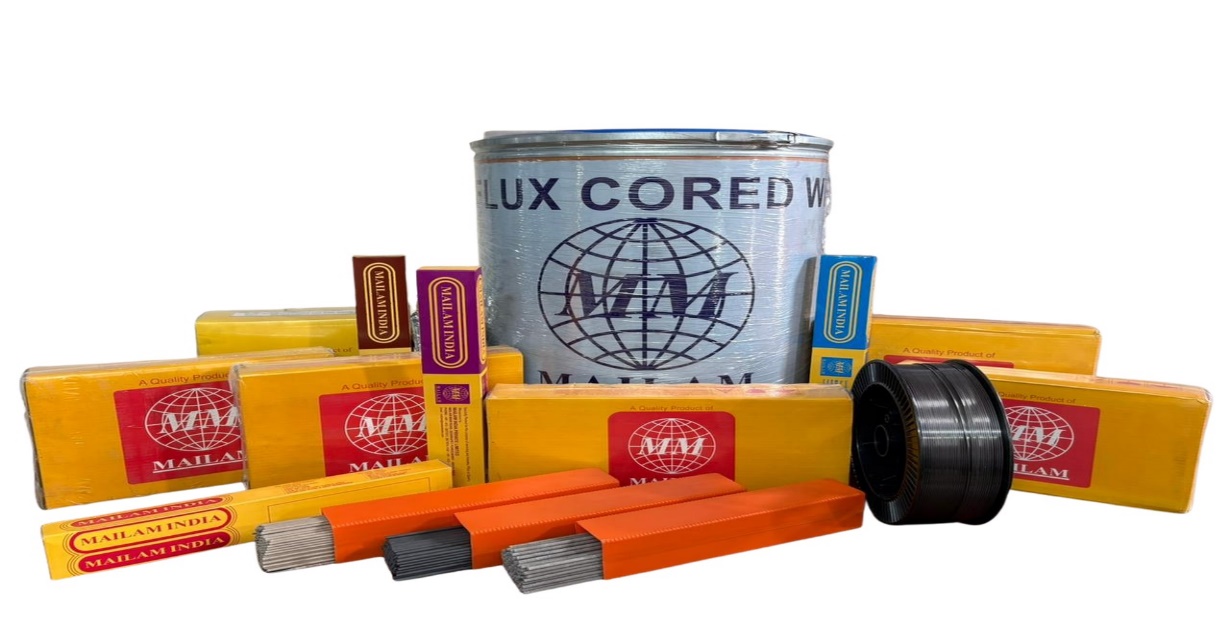
Self-manufactured FCAW wire
The formulation of various flux-cored wires is carefully designed to give a weld metal and microstructure that provides extra-long service life under high-stress abrasion, erosion, corrosion, impact and elevated temperatures.
Joining & anti-wear electrodes
For joining composite wear plates, a stainless-steel root run is laid in a double-V groove, then filled with multiple passes of a properly selected anti-wear electrode, a methodology refined over years at MUEL.
Enquire about grades →Download the product catalogue
Full overlay grade specifications, standard sizes and the complete parts range, in one PDF.